Levers and pulls
Door and cabinet hardware
Founded in 1978, we have grown into the largest privately owned PVD and CVD coating company in North America.
We run most major deposition technologies in our plant, from cathodic, pulsed and filtered arc to ion beam plating, reactive and magnetron sputtering, HIPIMS and PaCVD.
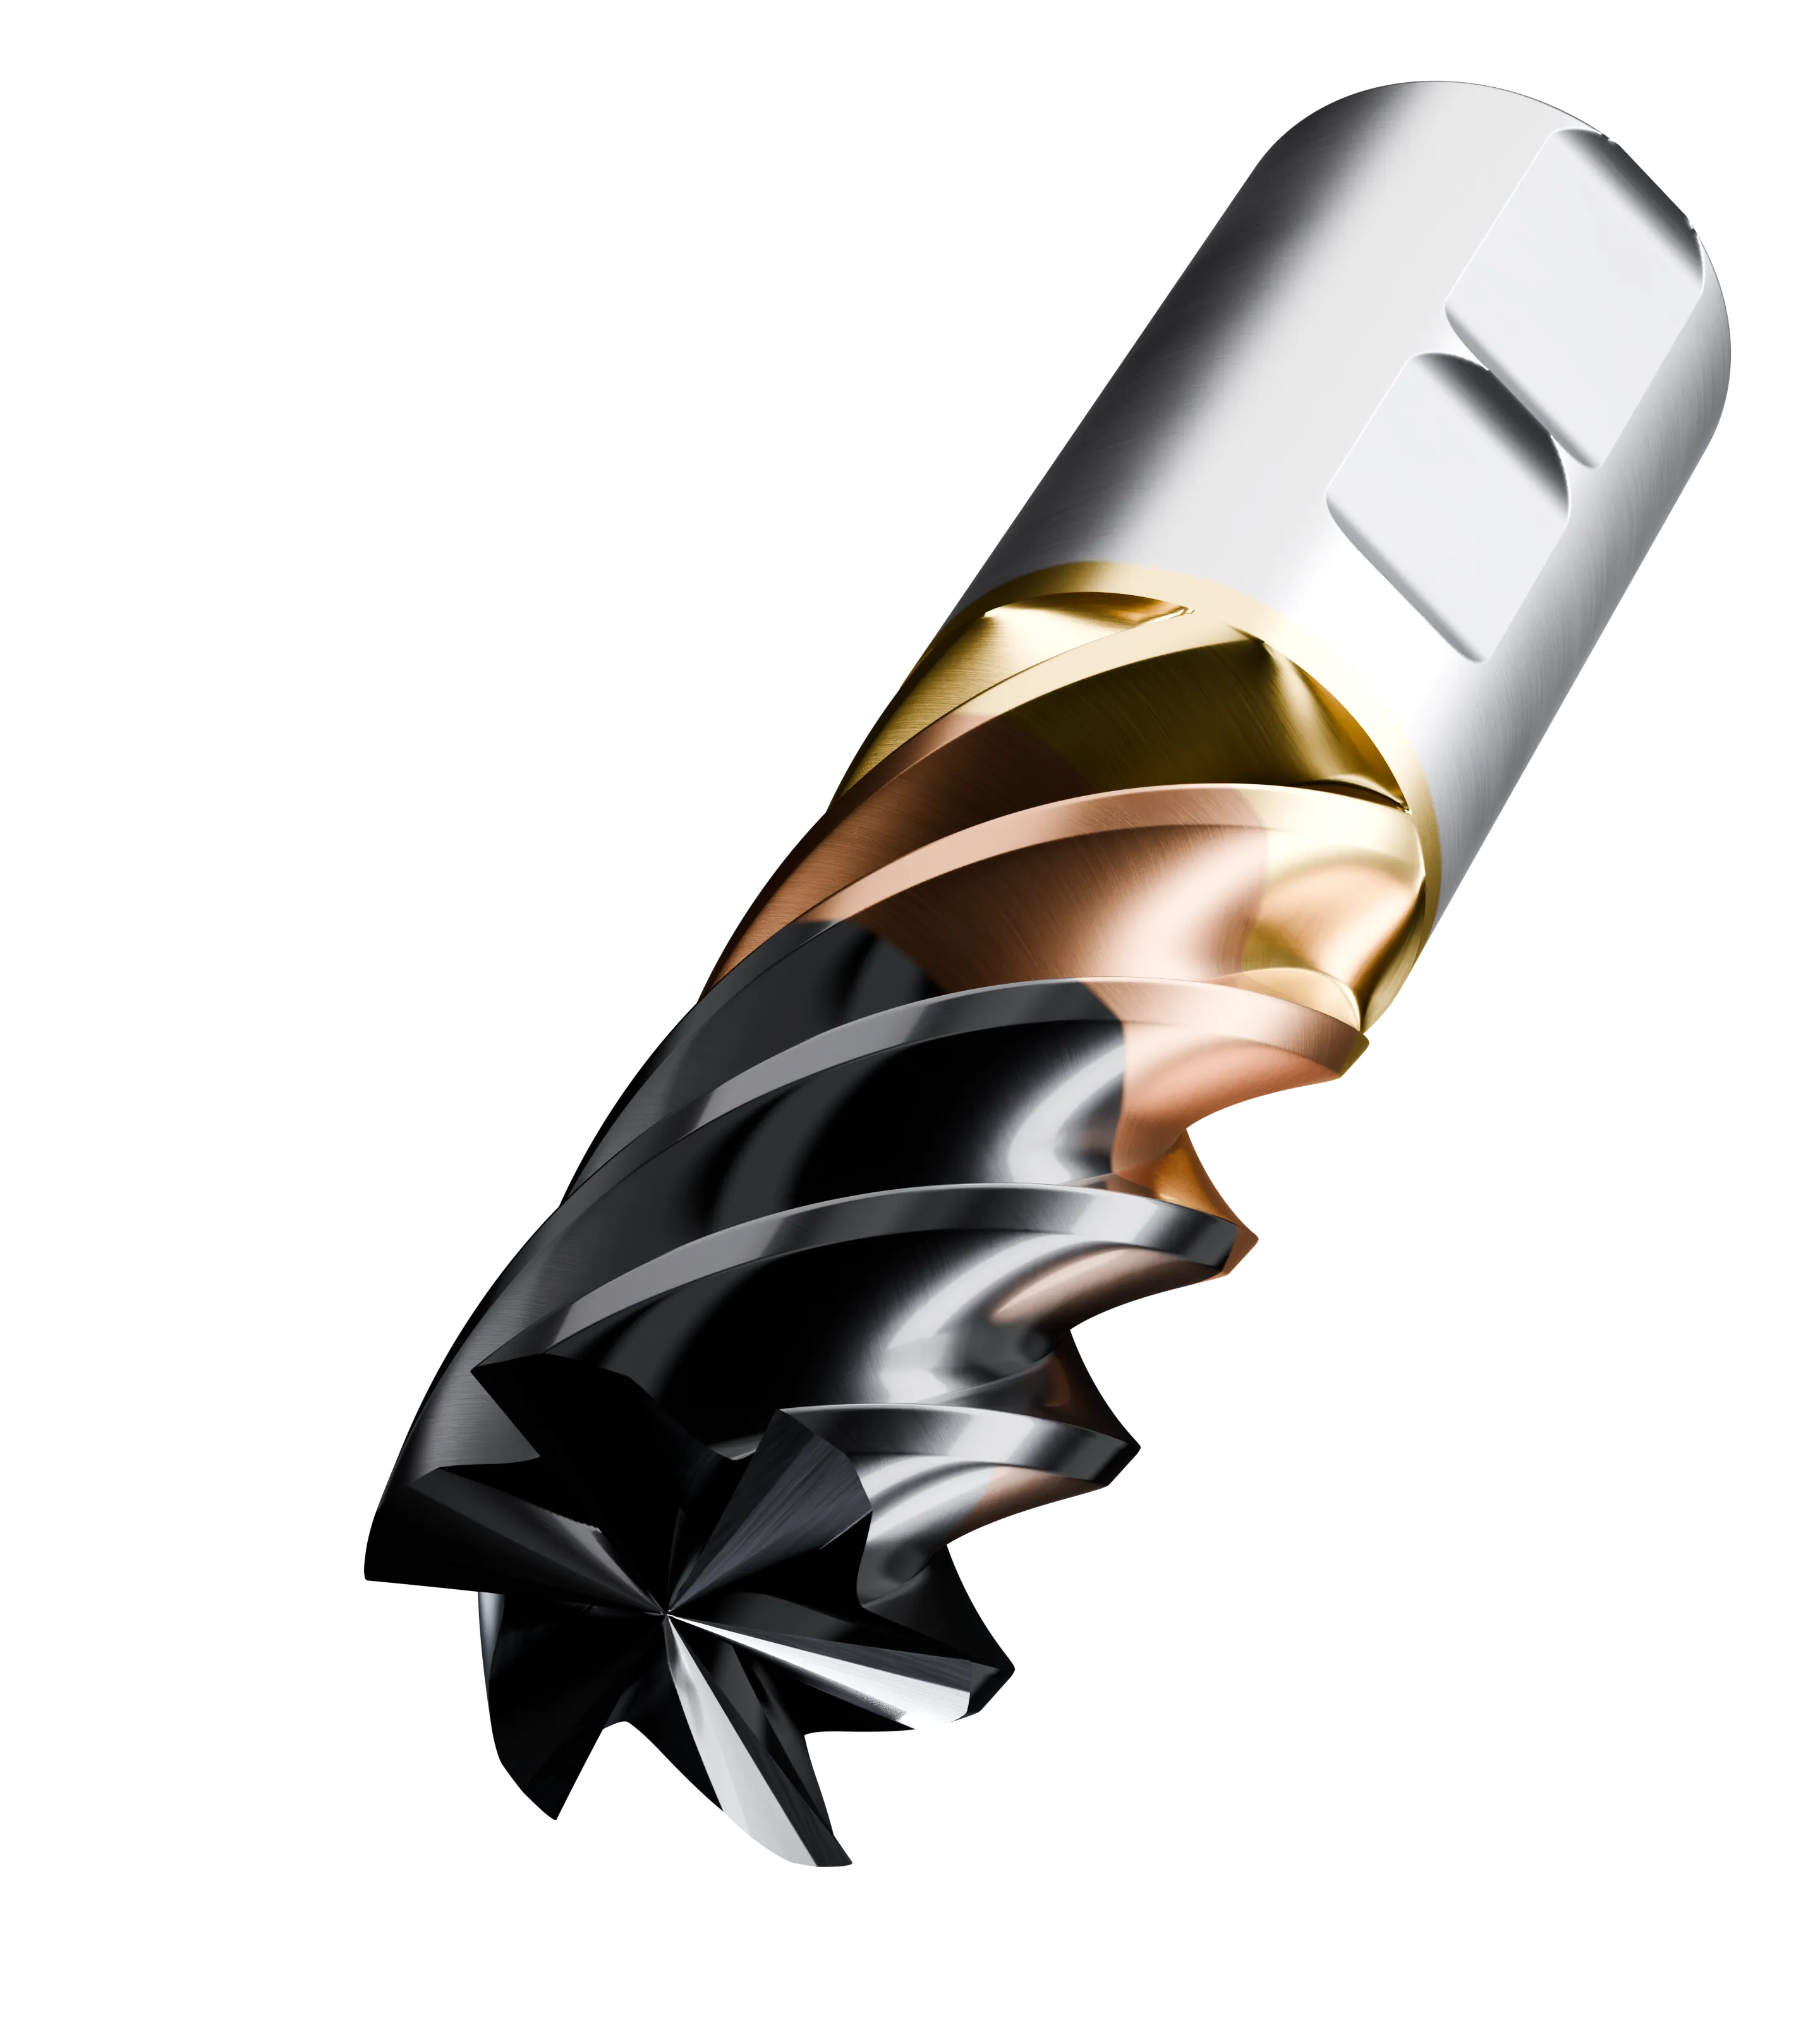
Low-temperature vacuum coatings applied between 320 and 800°F
High-temperature coatings formed at about 1925°F
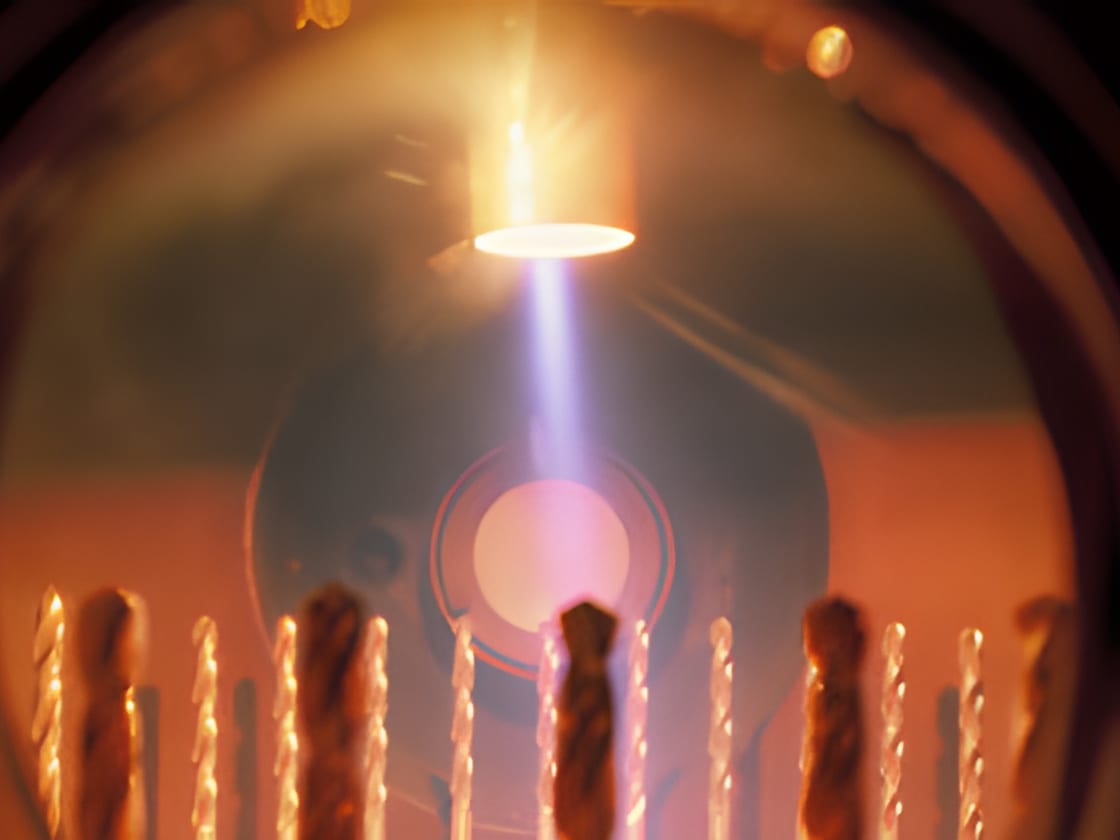
Most of our CVD and PVD units were built in our own plant, and our R&D engineers keep improving the processes while they develop new coating compositions.
Request a QuoteWe coat cutting tools, forming dies, molds and die casting tooling, along with medical devices, implants, decorative hardware and firearm parts.
Our storyOur standard line of general-purpose PVD coatings started with titanium nitride and now covers nearly 20 compositions for cutting, forming, molding and die casting tools.
We were the first PVD coating facility in North America certified to ISO 13485:2016, which complies with the FDA's 21 CFR Part 820, and most of our coatings are ISO 10993 compliant by third-party testing.
Request a QuoteBHMA and custom colors that come out smoother, brighter and harder than plating, with color held tight from cycle to cycle and year to year.
Door and cabinet hardware
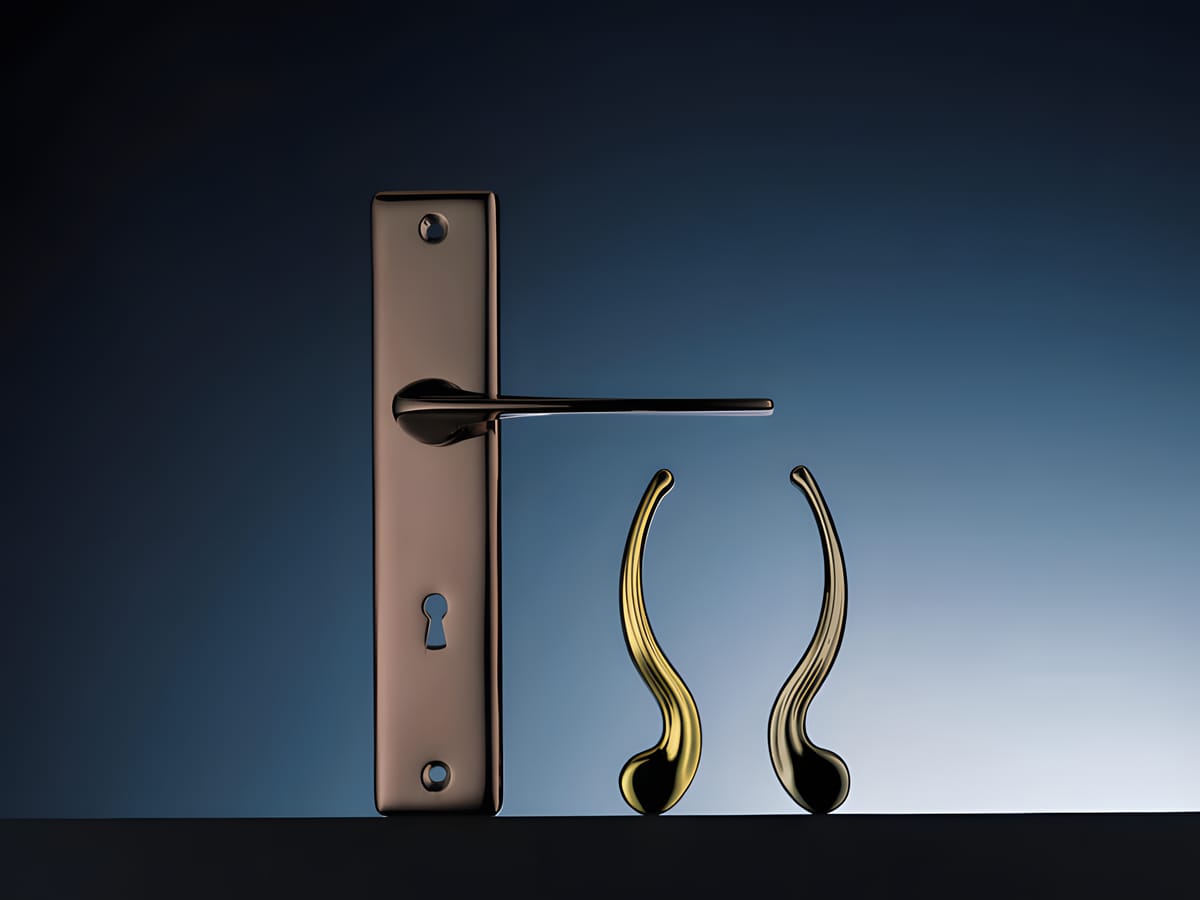
Door hardware on a backplate
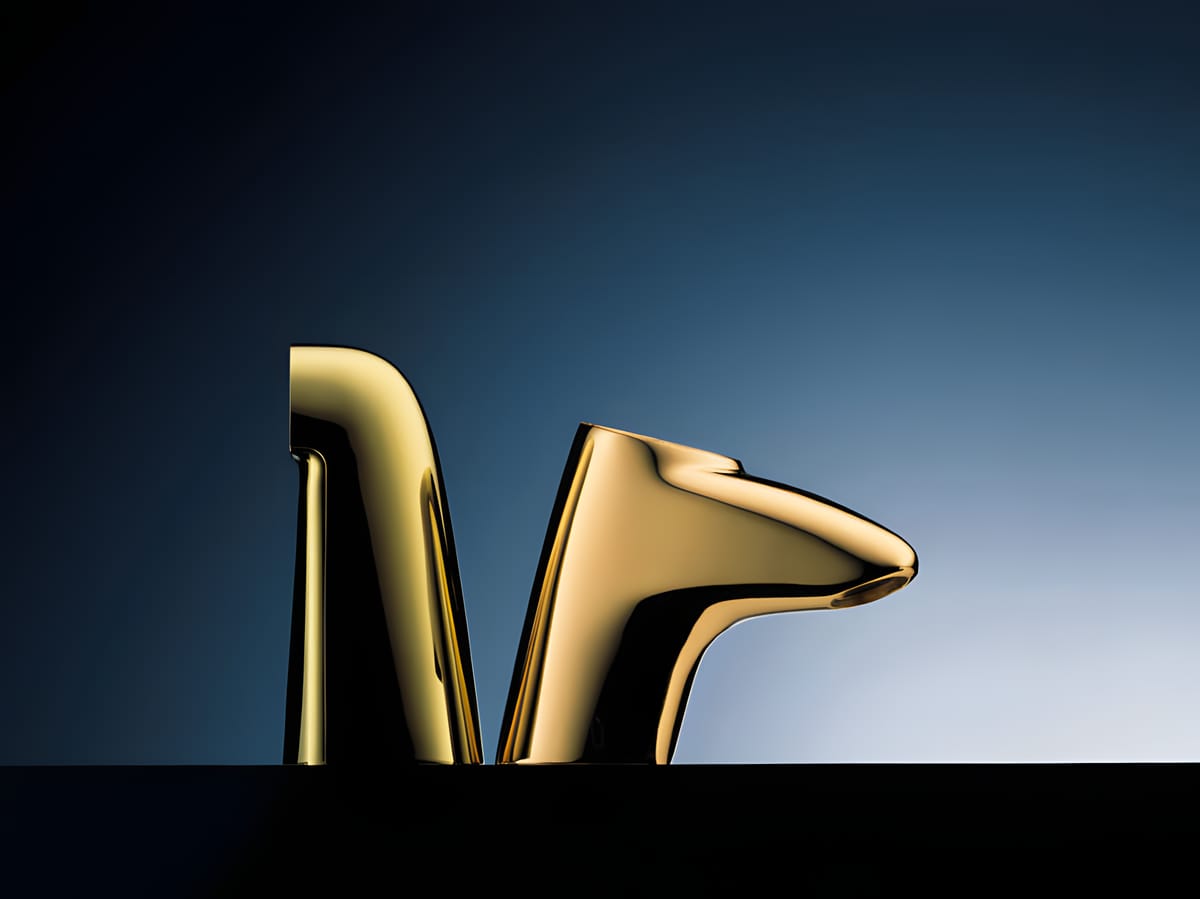
Kitchen and bath fixtures
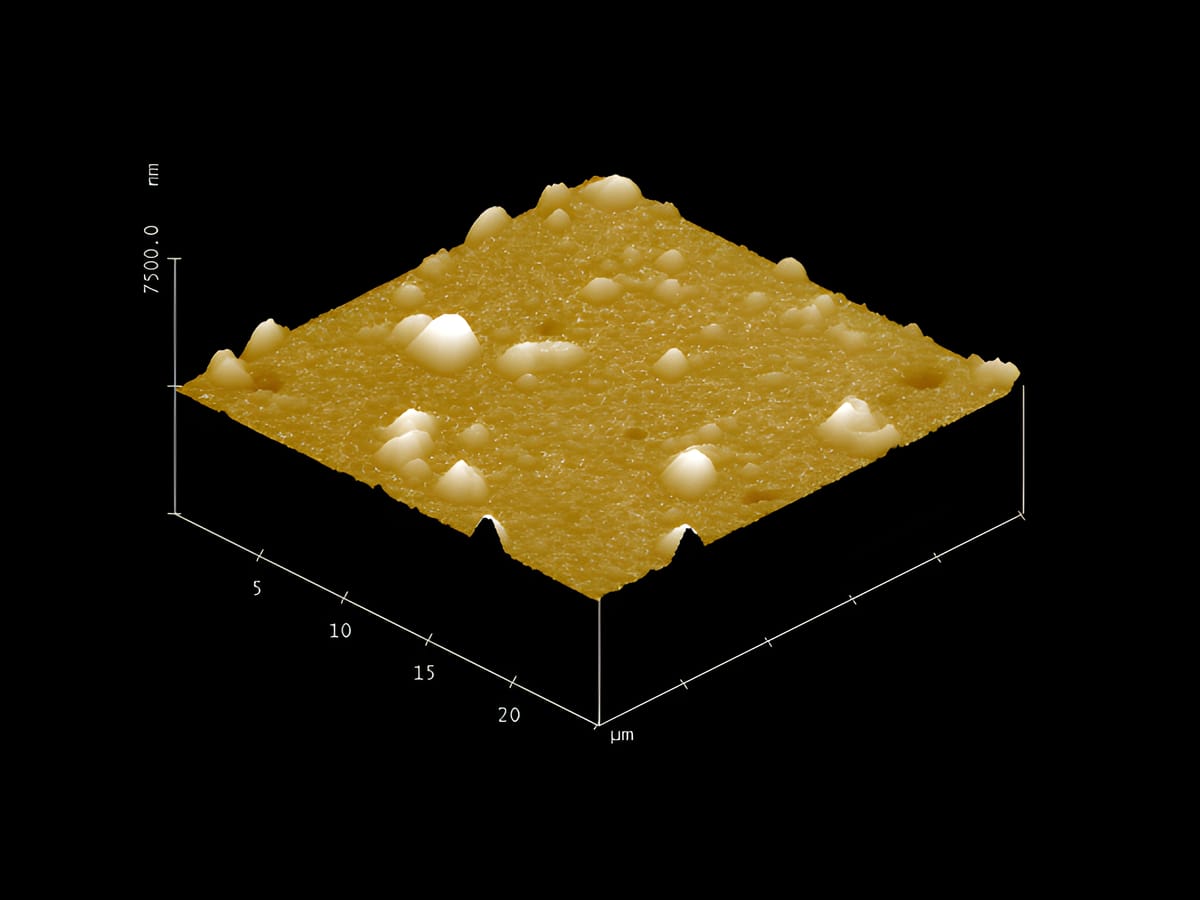
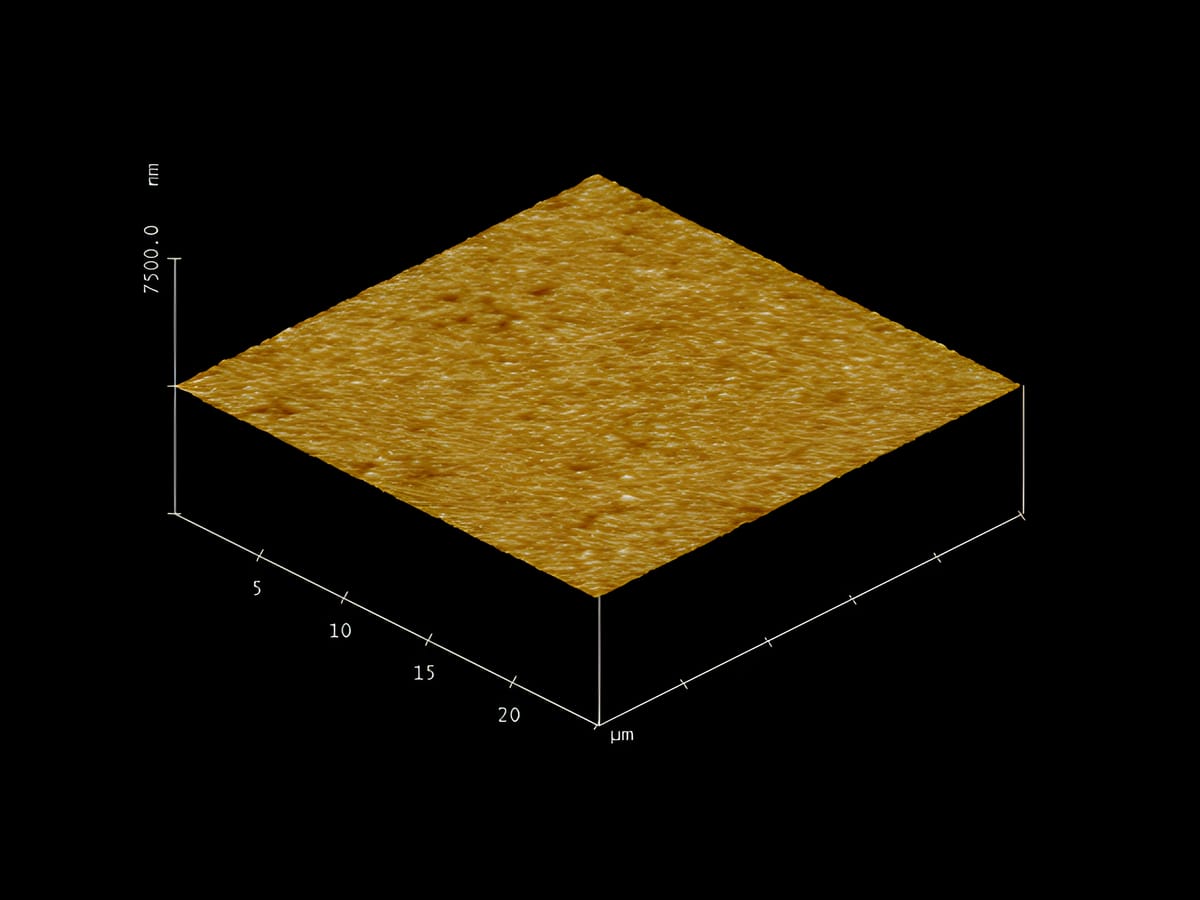
Replikote™ for polished molds
Replikote™ locks a polished finish under a hard, dense film because it filters out the macro particles that leave a typical PVD coating hazy.
That makes it suitable for lens molds and most optical work, with better release and less cleaning, and our Replikote™ C11 is the smoothest DLC coating on the market.
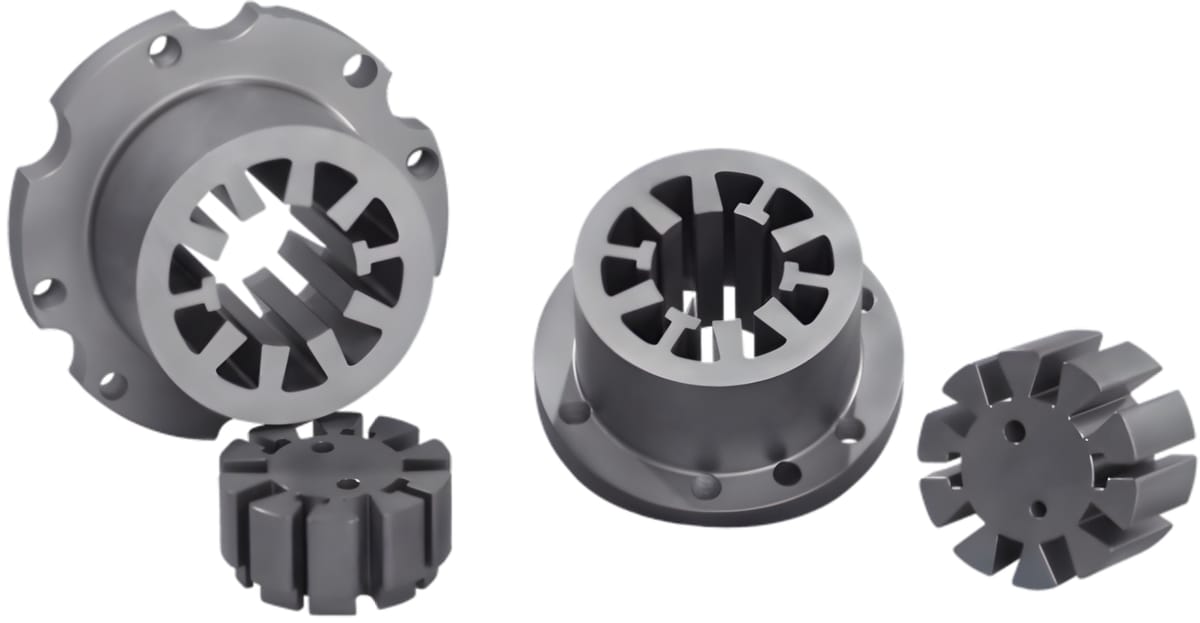
Plasma nitriding and PVD in one process, for severe metal forming and die casting, run at 932°F or below so tight tolerances hold.
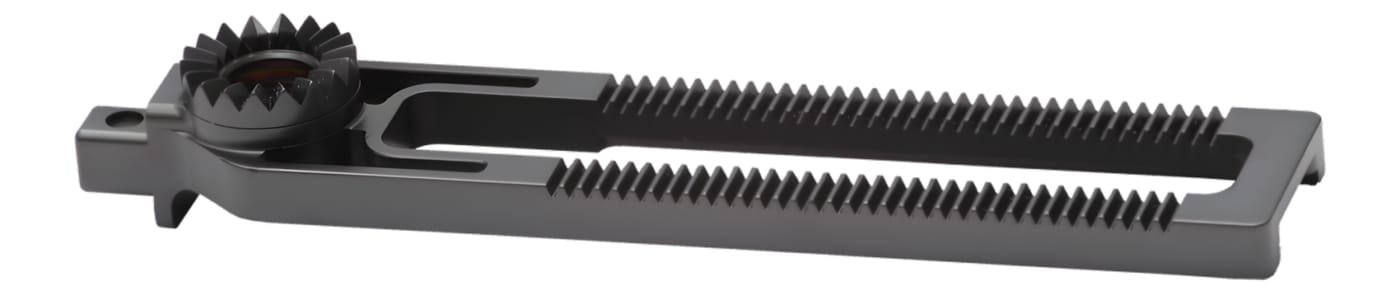
Our full range of DLC films, from Me-DLC to ta-C, pairs high hardness with low friction on engine parts, gears, molds and non-ferrous cutting tools.
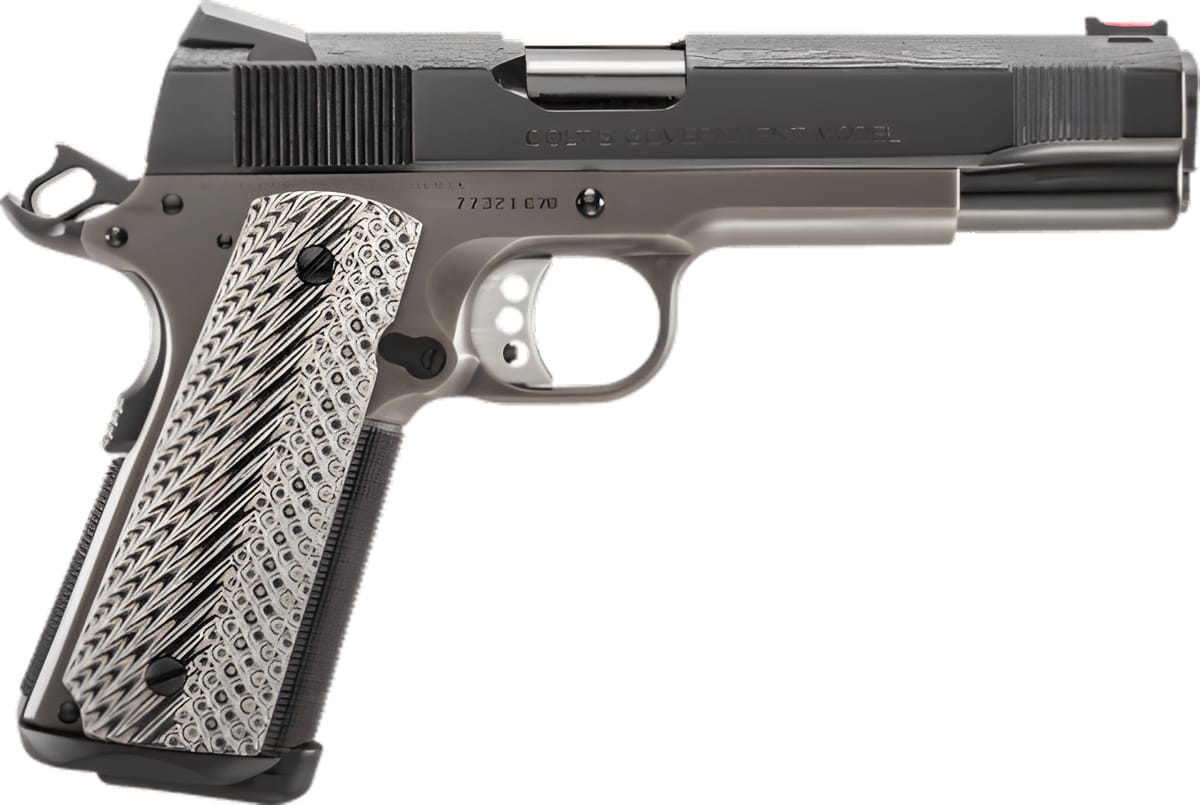
PVD, CVD and DCD coatings for slides, frames, barrels, suppressors and internal parts, offered to firearms manufacturers only.
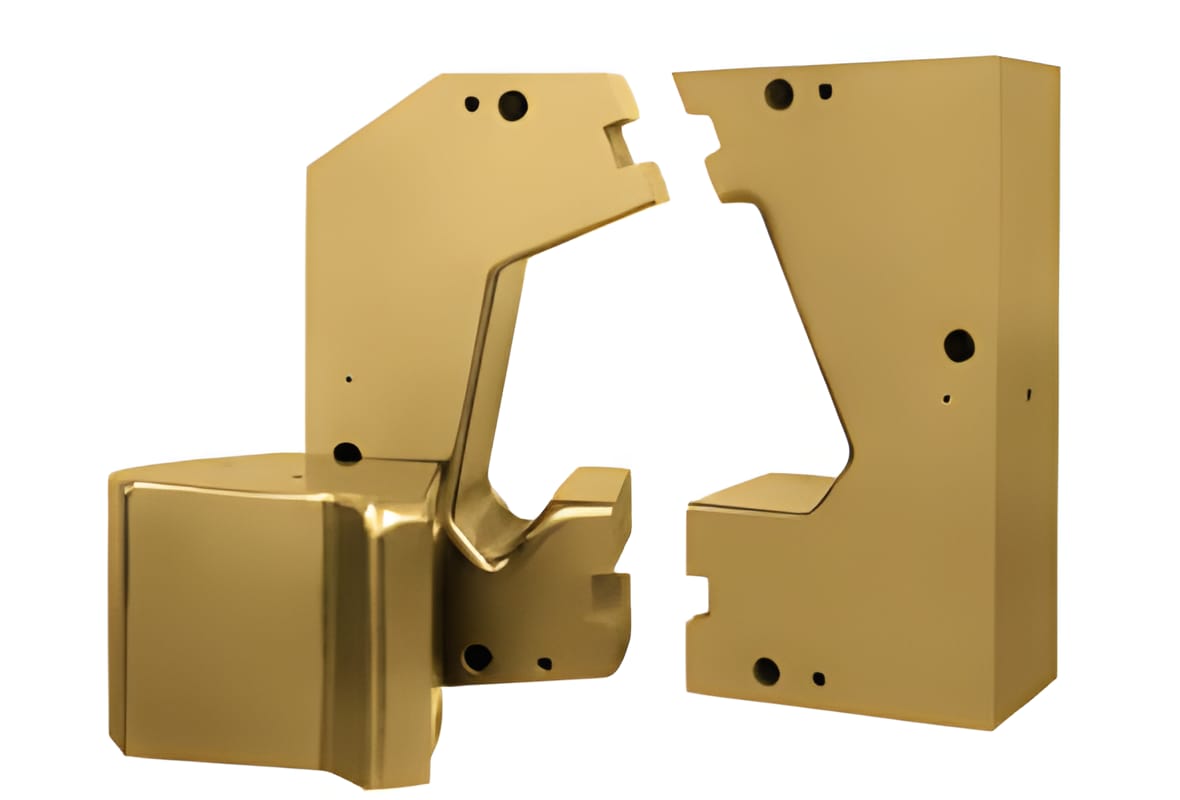
Titankote™ H, H+ and H+S bond chemically and metallurgically to the tool at about 1925°F, which stands up to the shearing stress on punches, draw dies, trim dies and cold heading tools.
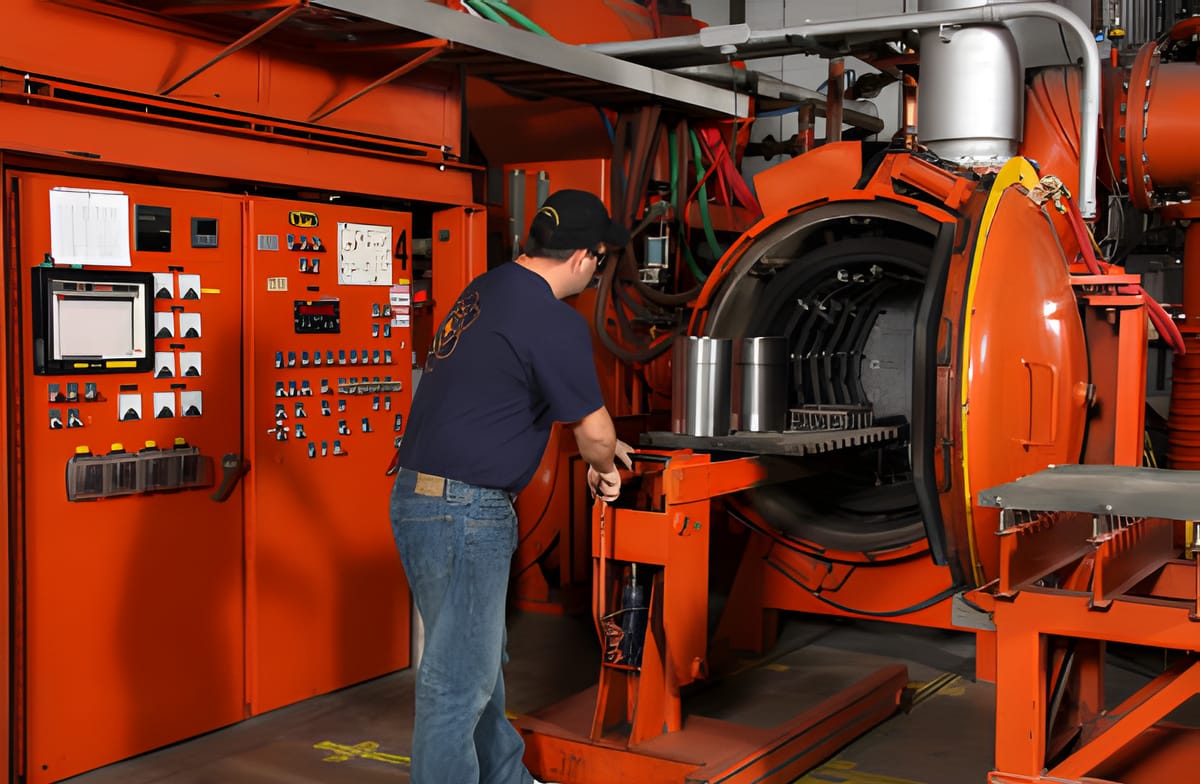
We harden tool steels, high speed steels and 400 series stainless at our Pennsylvania, Michigan and Kentucky plants, with 2, 6 and 10 bar quenching that leaves parts bright and free of scale.
Titankote™ B diffuses boron into the surface for a 1600 to 1900 HV case that resists heat, acids and cold welding on forging dies, extrusion dies, valves and nozzles.
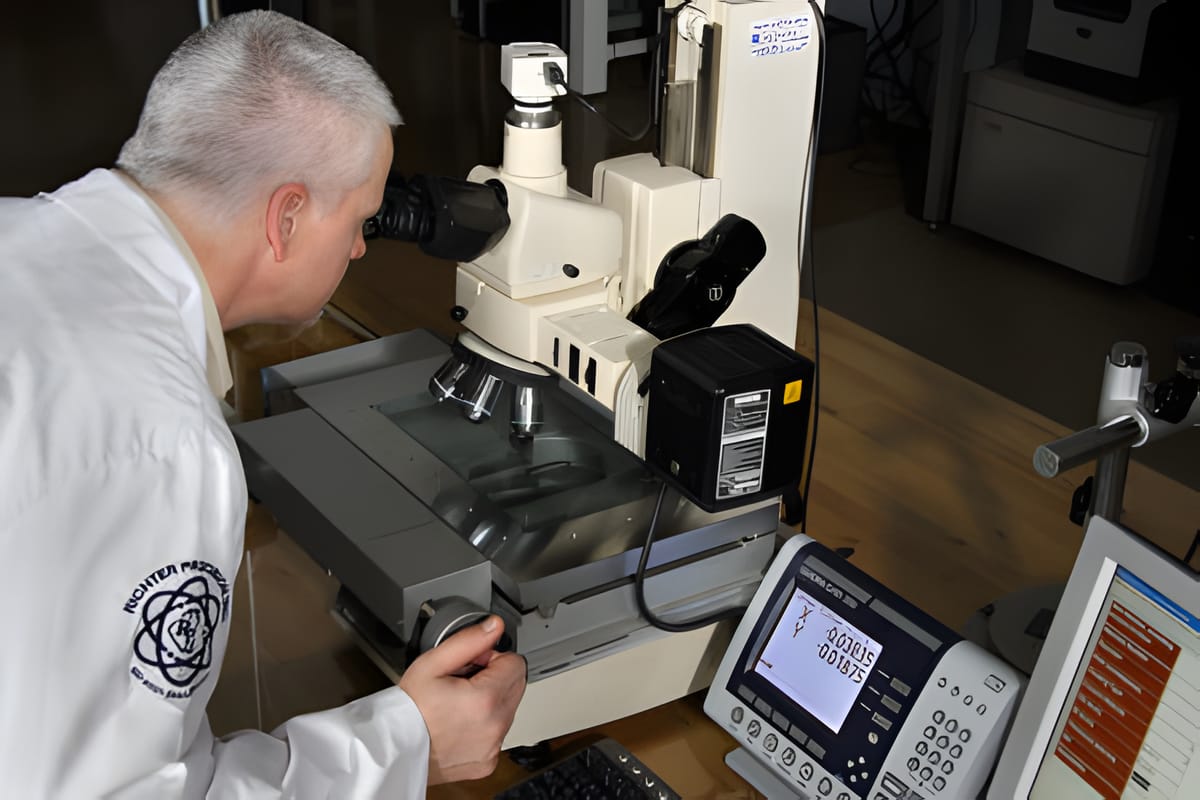
Our thin film and metallurgical lab runs SEM, nano-indentation, scratch adhesion, tribometer and film thickness tests, and it takes on commercial projects as well as our own R&D.
[ Titankote™ C10 · ta-C ]
5000–9000 HV
Micro-hardness of our hardest DLC film
[ Titankote™ C14 · C-DLC ]
0.06
Lowest coefficient of friction in our standard range
Data from lab samples, so results on your parts will vary with base material, surface condition and part geometry.
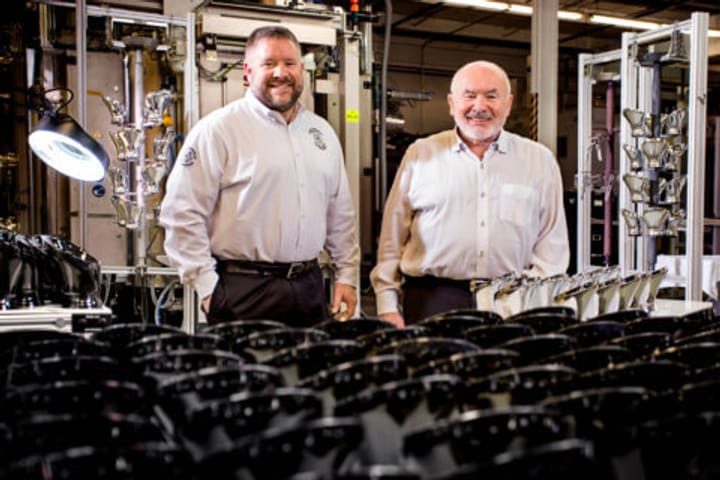
About Richter Precision
Hans Richter founded the company in 1978 to make and refurbish carbide inserts, and in 1981 he turned it toward CVD and PVD coating services.
We were the first in North America to use HIPIMS commercially, we pioneered commercial Super Lattice PVD and a wide range of DLC compositions, and every technician is retrained as each new process comes in.
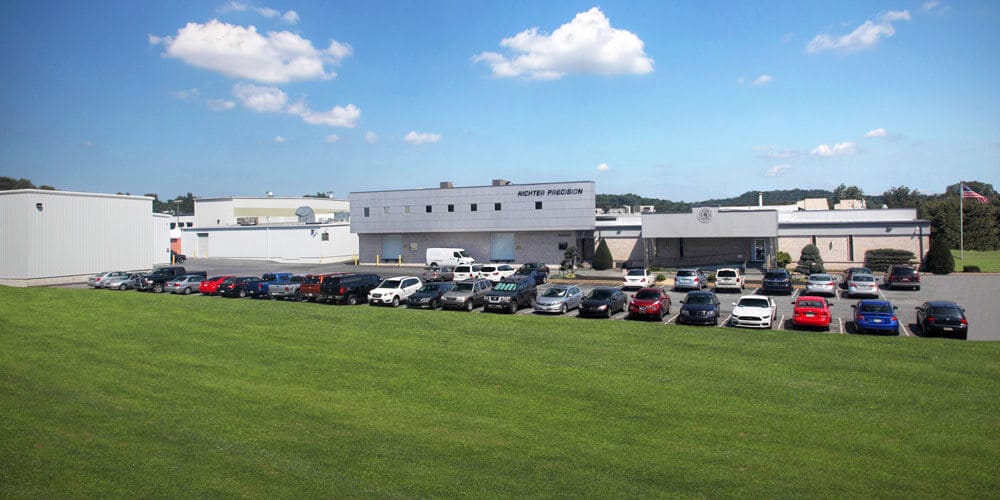
Headquarters, certified to ISO 9001:2015 and ISO 13485:2016
1021 Commercial Ave., East Petersburg, PA 17520
Vacuum heat treating, certified to ISO 9001:2015
Vacuum heat treating
Tell us what you need coated and what it has to survive, and we will recommend a coating and send a price.